Top Double Bottle Suction Machine for Efficient Production?
The efficiency of production lines has become crucial in today’s competitive market. The Double Bottle Suction Machine is transforming the way manufacturers operate. According to industry reports, the demand for such machines has surged by 30% over the past three years. This growth is driven by a need for increased productivity and reduced operational costs.
Manufacturers are looking for machines that offer precision and reliability. The Double Bottle Suction Machine stands out in this regard, utilizing advanced suction technology. This machine can efficiently handle multiple bottles simultaneously, ensuring swift packaging processes. Data from a leading industry analyst indicates that plants using these machines can boost their output by up to 40%.
However, companies must consider the investment and maintenance involved. Some users report challenges in adapting to the machine's operational nuances. Engaging with experienced technicians can alleviate these issues. Evaluating the pros and cons is essential for maximizing the benefits of the Double Bottle Suction Machine. Effective training can ensure that operators leverage its full potential, leading to improved production outcomes.
Understanding Double Bottle Suction Machines in Production
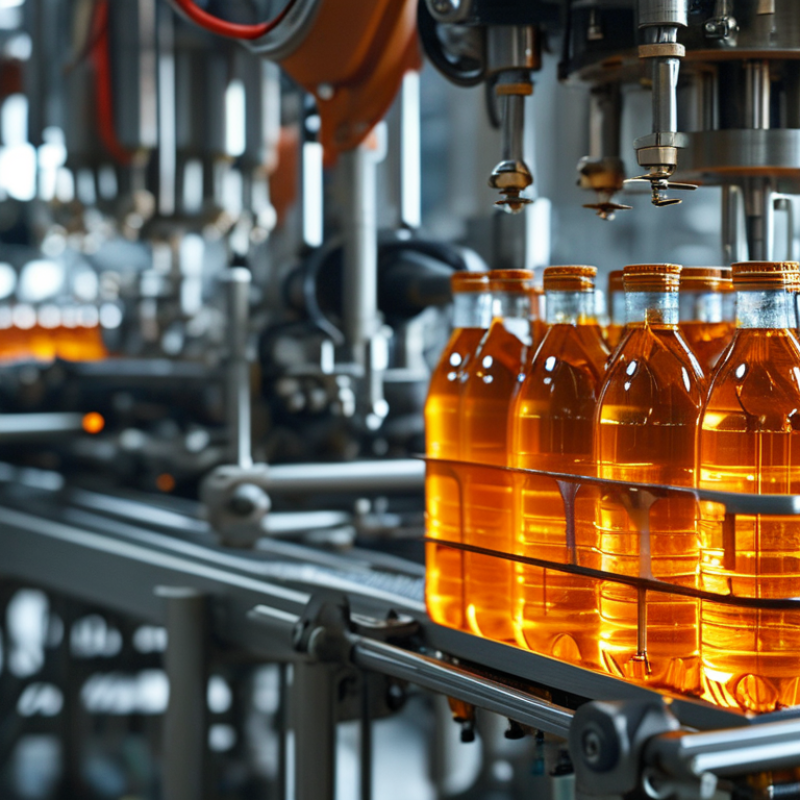
Double bottle suction machines have become essential in various production settings. They streamline the process of handling and transporting liquid-filled bottles. Understanding how these machines work can significantly enhance operational efficiency.
These machines utilize dual suction capabilities to grip and lift two bottles simultaneously. This design minimizes the time spent on loading and unloading, allowing for a smoother production flow. However, operators must be trained in their use to avoid mishaps. Misalignment can lead to dropped bottles, causing waste and potential safety hazards.
While the technology is effective, maintenance issues can arise. Regular checks are necessary to ensure the suction cups are intact. Any wear and tear can reduce performance. Additionally, a learning curve exists for new users. Understanding the machine's nuances is crucial for optimal results. Observing and addressing these challenges can contribute to a more effective production process.
Key Features of Top Double Bottle Suction Machines
Double bottle suction machines play a crucial role in manufacturing sectors, especially in the beverage and pharmaceutical industries. These machines enhance production efficiency significantly. The demand for such equipment has surged, with a projected market growth rate of 5.6% annually, according to recent industry reports.
Key features of leading double bottle suction machines include:
- High suction power
- Adjustable speed settings
- Energy-efficient operations
Many models offer dual suction capabilities, allowing for picking and placing two bottles at once. This can lead to a remarkable reduction in cycle time, thus increasing overall productivity. Additionally, these machines often come equipped with
user-friendly interfaces, which minimize the learning curve for operators. However, some users report maintenance challenges, indicating a need for better design in accessibility.
Furthermore, the reliability of these machines is under constant scrutiny. While they promise higher outputs, the frequency of unexpected downtimes can detract from their efficiency. A balance between automation and manual oversight may be necessary. Regular training and updates can help mitigate some of these issues. Reports suggest that operators who understand machine intricacies can dramatically improve overall performance.
Benefits of Using Double Bottle Suction Machines for Efficiency
Double bottle suction machines are becoming vital in modern production lines. These machines streamline operations, increasing overall efficiency. They handle multiple bottles simultaneously, which reduces cycle time. In a fast-paced environment, every second counts. For businesses, this means faster production rates and improved output.
The benefits of using double bottle suction machines extend beyond just speed. They minimize manual labor, which can lead to fewer errors. An automated system often produces more consistent results. Workers can focus on quality control and troubleshooting instead. However, some may argue that the reliance on automation has its downsides. Potential machine malfunctions can disrupt the workflow. Frequent maintenance is crucial to ensure reliability.
Investing in this technology also enhances safety. Workers are less exposed to repetitive strain injuries. Yet, many companies struggle with the initial cost of these machines. Evaluating return on investment is essential. Balancing efficiency gains against setup costs requires careful thought. A well-planned implementation can yield significant long-term benefits, reinforcing production efficiency.
How to Maintain Double Bottle Suction Machines for Optimal Performance
Maintaining double bottle suction machines is crucial for optimal production performance. Regular maintenance prevents inefficiencies and extends the equipment's lifespan. Studies show that machines undergo a significant reduction in productivity when not properly maintained. For instance, data indicates that poorly maintained suction machines can lose up to 25% of their efficiency over time.
Routine cleaning is essential. Clogged filters can lead to operational failures. It’s recommended to clean filters weekly to keep the suction power consistent. Furthermore, lubricating moving parts regularly can prevent wear and tear. Experts highlight that businesses often overlook lubrication, which can result in increased operational costs due to frequent repairs.
Another aspect is checking for wear and tear on hoses and seals. Small leaks can drastically affect performance. A small leak might seem insignificant, but it can reduce suction capabilities. Research shows that even minor issues can lead to major problems when ignored. Regular inspections should be part of a maintenance schedule. Mindful maintenance can enhance the effectiveness of the machine and contribute to a more efficient production line.
Comparing Popular Brands of Double Bottle Suction Machines in the Market
In recent years, the demand for double bottle suction machines has surged. These machines enhance production efficiency in industries like food and beverage and pharmaceuticals. Market research indicates that the global suction machine market is projected to grow at a CAGR of 6%, reaching approximately $1.2 billion by 2025. This growth reflects the increasing need for advanced packaging solutions.
When comparing popular brands, it's essential to look beyond flashy features. Reliability and ease of maintenance are critical. Industry data highlights that machines with user-friendly interfaces lead to a 15% reduction in downtime. Moreover, machines that offer customizable suction settings provide flexibility for various bottle shapes and sizes, which is invaluable in diverse production environments.
However, not all machines are created equal. Some models struggle with inconsistent suction power, leading to wasted materials. Manufacturers often miss this crucial aspect during testing. Real-world performance may vary from claimed specs, which can impact overall production efficiency. Buyers need to weigh these factors carefully before making a decision, as the right equipment is vital for long-term success in their production lines.